Quick answer: the finished plate begins with controlled casting inputs
A cast-iron weight plate normally starts with a released drawing and pattern, followed by mould preparation, metal melting and composition control, pouring, cooling, shakeout, gate and flash removal, cleaning, any specified machining, weight and dimensional checks, surface finishing, marking and packing. The exact route varies by plate design and foundry, so a buyer should approve the product-specific process rather than assume every cast plate follows one recipe.
ChinaFreeWeight is a factory partner for OEM, ODM, Custom Logo, Private Label and Bulk Supply projects. We connect the approved plate model to samples, process records and final inspection, while stating clearly which operations are performed by the selected production route. A staged photograph or one molten-metal video is not proof that a complete shipment meets the drawing.
Freeze the drawing, pattern and weight logic before metal is poured
The drawing should separate functional dimensions from decorative geometry. Outside diameter, bore, thickness, hub or rim lands, grip openings, lettering, mould-release angle, parting line and machining allowance all affect the pattern and mould. Nominal mass must be planned with material density and later finishing in mind; it cannot be corrected responsibly by adding random paint or leaving uncontrolled flash.
Approve the full denomination range, not only the largest plate. A light plate may use a different section or cavity layout, while a heavy plate may cool differently. Record pattern identity, cavity or tool reference, artwork revision and which surfaces will remain as-cast, be ground, or be machined. These records protect reorders when a pattern is repaired or replaced.
Treat sand moulding and metal preparation as separate controls
Treat sand moulding and metal preparation as separate controls
Sand casting uses a pattern to form the cavity, with a gating and feeding system that lets molten iron enter and solidify. The American Foundry Society explains that sand is widely used for moulds and cores, while the US EPA foundry process description separates mould production, melting, pouring, cooling, shakeout and finishing. Those sources explain the route; they do not certify a gym plate.
The purchase specification should identify the agreed cast-iron grade or property basis and the evidence expected from the production source. ISO 185 classifies grey cast irons by strength or hardness options, but it does not select a grade for every weight plate. Material identity, charge control and any test request belong to the specific drawing and order.
Pouring and cooling create risks that finishing cannot hide
Pouring and cooling create risks that finishing cannot hide
Melt condition, mould condition, filling path and cooling influence whether the casting reproduces the intended geometry. Visible cold shuts, incomplete fill, inclusions, shrinkage indications or displaced mould features should not be disguised under filler or a heavy coating. The defect catalogue and disposition route must be agreed before production pressure makes appearance the only release criterion.
Do not turn a generic process description into a universal temperature, cooling time or defect allowance. Foundries use different equipment and control plans. Ask for the actual first-piece record, lot identity and inspection points, then compare representative castings from across the run rather than a specially prepared display sample.
Cast-iron plate process-control matrix
| Stage | Buyer must define | Evidence to retain |
|---|---|---|
| Drawing and pattern | Functional geometry, release angle and artwork | Released drawing and tool identity |
| Mould and metal | Process route and material basis | Lot and first-piece records |
| Pour and cool | Visible defect and disposition rules | Casting inspection record |
| Fettling | Edges, flash and protected features | Approved surface reference |
| Machining | Features, datums, limits and allowance | Dimensional report |
| Finish and release | Coating, marking, packing and sampling | Signed sample and final report |
Separate shakeout, fettling and machining decisions
Separate shakeout, fettling and machining decisions
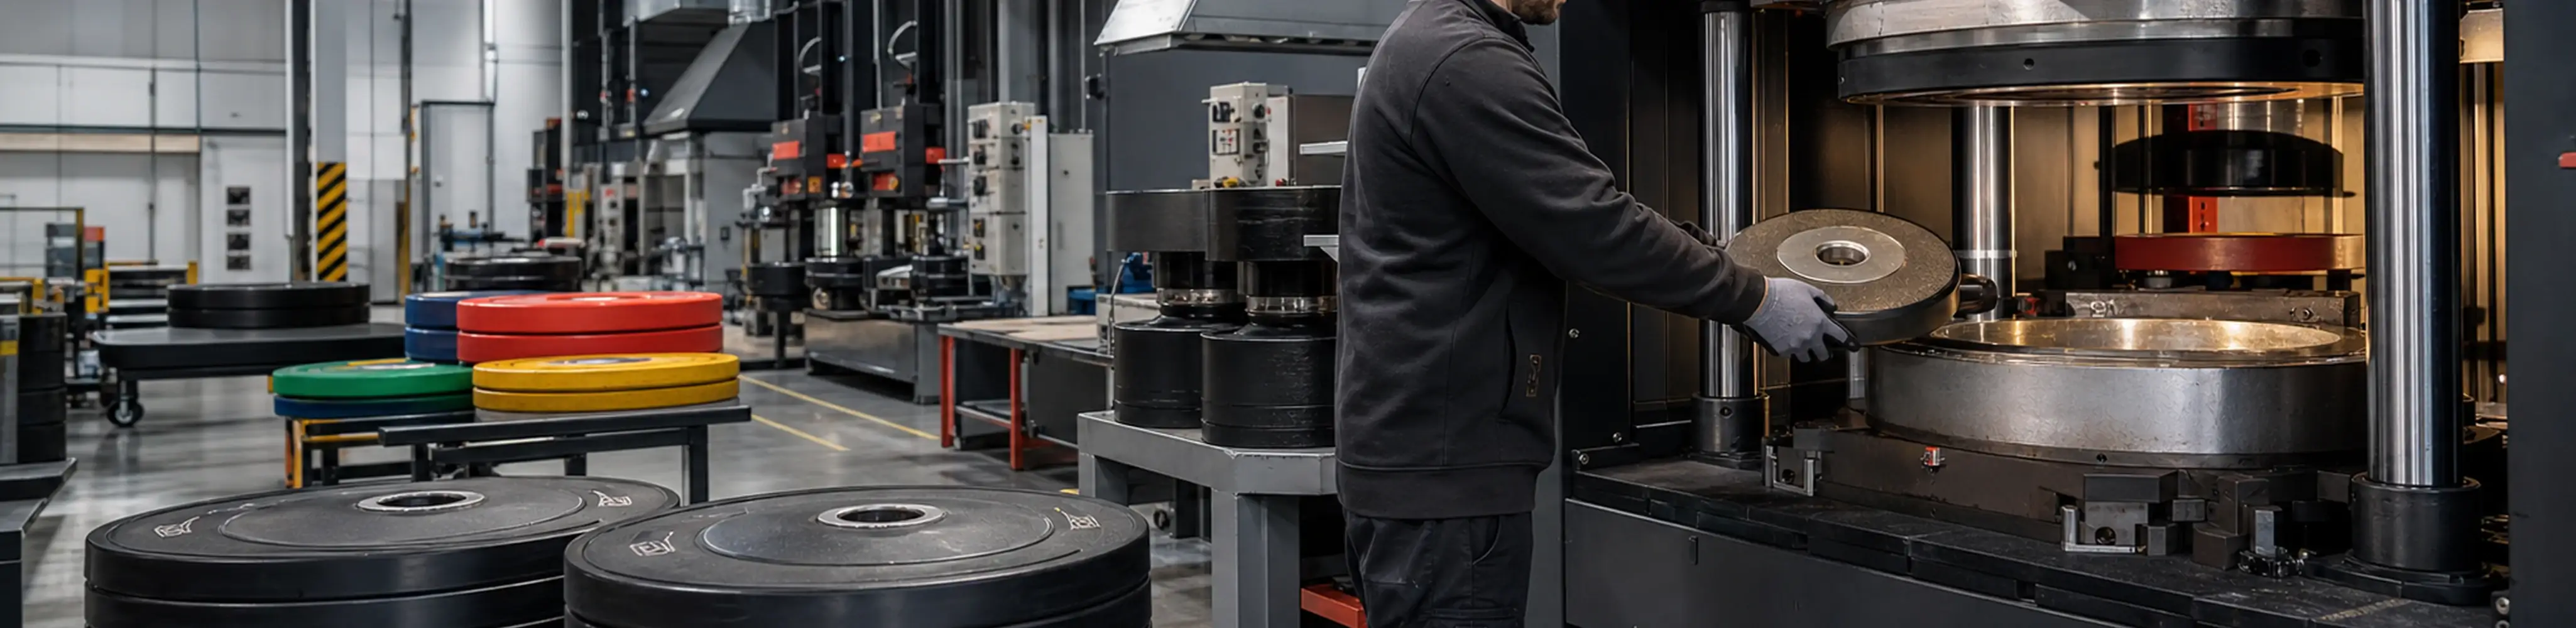
After cooling, the mould is broken away and sand is removed. Gates, risers, parting-line flash and sharp projections are cut or ground, and the surface may be blast-cleaned. Fettling should leave safe, repeatable edges without cutting into a functional rim, grip opening or weight mark. A smooth-looking plate can still have an incorrect bore or thickness.
Machining is a drawing decision, not a synonym for quality. The bore, hub face, rim or selected faces may be machined when the model requires tighter geometry or a defined contact. ISO 8062-3 provides language for casting tolerances and machining allowances; buyer and manufacturer must still identify the controlled features and acceptance limits for the actual plate.
Finish, markings and packaging complete the product, not the casting
Finish, markings and packaging complete the product, not the casting
Bare, painted, powder-coated or otherwise finished plates need a compatible surface preparation and a defined appearance reference. Finish cannot repair incorrect mass, bore geometry, cracking or unsafe edges. Keep coating build away from fit-critical areas unless the approved drawing includes it, and preserve readable weight identification after the selected process.
Custom logos can be cast, filled, printed or applied by another approved method, depending on the design. Review relief depth, location, contrast and contact points on a production-equivalent sample. Private-label cartons must identify the correct denomination and protect faces, rims and bores without presenting generated editorial imagery as a real customer order or factory inspection record.
Release the bulk order through linked process and product evidence
Release the bulk order through linked process and product evidence
At sample approval, check model identity, mass, outside diameter, thickness, bore and mating fit, flatness or functional contact, edge condition, markings, finish and packing as separate characteristics. Retain the signed drawing, physical reference, photographs, measurement method and artwork. A passing weight reading does not release a rough bore, and a clean finish does not release an underweight plate.
For bulk inspection, spread samples across denominations, production periods, mould cavities or pattern positions and cartons. Record individual findings and hold unexplained mixed revisions. Require review after material, pattern, gating, machining, finish, artwork or subcontractor changes. Send ChinaFreeWeight the range, unit system, target use, logo files, packing needs and destination so the factory route can be reviewed before quotation and sampling.
Ten checks before approving production
- Identify every denomination and drawing revision.
- Name the iron grade or agreed property basis.
- Record pattern, cavity and artwork identities.
- Define as-cast, ground and machined surfaces.
- Agree visible defect and sharp-edge criteria.
- Measure mass and geometry as separate gates.
- Approve coating and marking on finished samples.
- Sample across time, tooling positions and cartons.
- Protect bores, rims and faces in export packing.
- Require reapproval after material or process changes.
Continue the weight-plate specification
- View the cast-iron plate
- Browse commercial weight plates
- Compare plate materials
- Choose a cast-iron finish
- Set plate weight acceptance
- Plan pre-shipment inspection
- Send the manufacturing brief
Frequently Asked Questions About Cast-Iron Plate Manufacturing
Are all cast-iron weight plates sand cast?
Sand casting is common, but buyers should confirm the actual process for the quoted model. The category name alone does not prove a moulding route or quality level.
Does a machined plate automatically weigh more accurately?
No. Machining can control selected geometry and remove material, but mass accuracy still depends on the casting target, correction method, measurement plan and written tolerance.
Why is there a line around a cast plate?
It may be the mould parting line. Its position and finishing should match the approved sample and must not leave unsafe flash or interfere with stacking and handling.
Can paint hide casting defects?
Paint can change appearance but must not be used to conceal cracks, incomplete fill, unsafe edges or wrong geometry. Product acceptance should occur before and after finishing.
What changes should trigger a new sample?
Changes to material basis, pattern, cavity, gating, machining, coating, artwork or production source should be reviewed for affected characteristics and reapproved as agreed.
Build the process around the approved plate
Share the plate range, drawings, material basis, finish, Custom Logo, Private Label packaging and inspection needs. ChinaFreeWeight will review an OEM, ODM and Bulk Supply route for the selected model. Discuss your plate project.